The shift to high-solids and solvent-free formulations is, quietly, a mixing-equipment story: a batch tank that relied on solvent to cut viscosity is replaced by an inline device that blends at whatever viscosity the chemistry now has. For two-component (2K) epoxies, urethanes and sealants the mixer is even more central — the reaction starts when the components meet, so the mixer is the process. What follows is how we segment the duty and pick geometry, with the spec limits stated plainly.
Two Different Jobs: Distribution vs Deagglomeration
This is the round's research finding, and it sets honest expectations: peer-reviewed CFD work on cross-bar (SMX-type) elements shows that for liquid–liquid systems the droplet size a static mixer produces is set by the local energy dissipation inside the element lattice — the mixer disperses droplets, but nothing in its mechanism breaks solid pigment agglomerates (Imperial College London, DNS study of surfactant-laden liquid–liquid flow in an SMX mixer). So the division of labour is fixed: the mill deagglomerates, and the static mixer distributes the already-milled millbase uniformly through letdown, tinting and delivery. Promising a mixer will "disperse pigment" is the fastest way to buy the wrong machine.
Match the Element to the Regime
| Duty | Regime & viscosity | Geometry that fits | Spec anchor |
|---|---|---|---|
| 2K epoxy / PU / polyurea at the dispense gun | Laminar, paste to 10⁵ cP | Helical-element disposable nozzle; components combine just before application (Hernon's dispensing line is built exactly this way) | Cure stays in the nozzle — treated as a consumable |
| 100% solids coatings on the production line | Laminar, 1–10,000 cP | Cross-bar SX type | σX ≤ 1–5% with 4–6 elements; 2–5 velocity heads per element |
| Low-viscosity letdown and fine emulsification | Turbulent, ≤ 100 cP, clean stream | Corrugated-plate SV type | Sub-5 µm dispersion — but no fibres, no suspended solids above 0.5 mm |
| Pastes and hotmelts beyond 10,000 cP | Deep laminar, to 10⁶ cP | Helical SK type | Highest-viscosity construction in our range |
The table is deliberately blunt about limits. The SV plate mixer earns its superb dispersion numbers only inside a narrow window — our own datasheet excludes it above 100 cP, with fibres, or with solids over 0.5 mm — and pushing it into high-solids coatings duty is a plugging complaint waiting to happen. Element choice is also the first defence against clogging and fouling.
Ratio Accuracy Is the Meter's Job; Variance Is the Mixer's
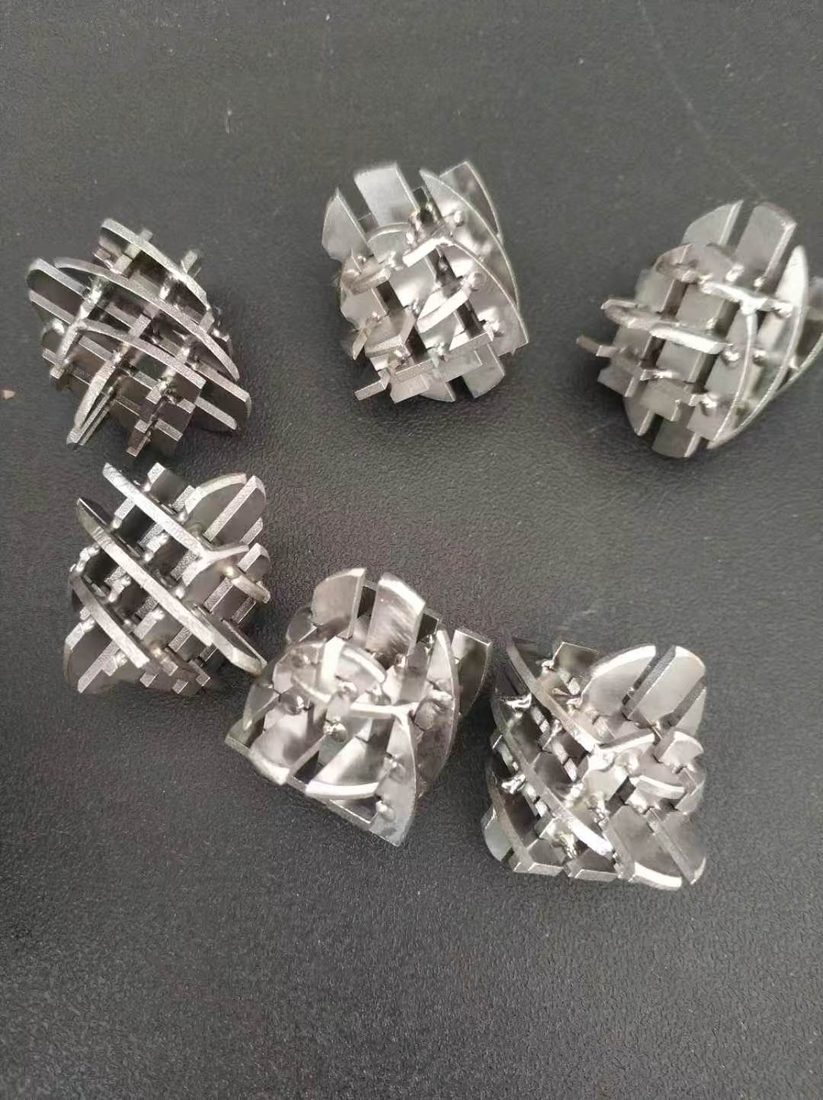
In 2K work it pays to keep the two machines honest and separate. Metering pumps own the ratio; the mixer owns uniformity. What the ratio does own inside the mixer is difficulty: a large viscosity ratio between components stretches the length needed to reach the same non-uniformity, which is why both component viscosities — not the blended average — belong on the datasheet you send for quotation. On the dispensing side the industry long ago accepted the consequence of the cure clock: nozzles with internal helical elements are specified, sized and then thrown away, because the cured adhesive stays inside them. An inline production mixer inverts that economics — no consumable, but a flush protocol, warm-jacketed housings, and quick element access are part of the purchase, not extras.
Before You Shortlist
Size the duty honestly with the sizing procedure, budget the pump for the element count using the per-element head ratings, and pick metallurgy from the materials comparison — 316L covers most coatings plant duty, and plastics win where solvents dictate. For pilot lines and colour-matching work, our transparent sight-glass mixer lets you watch the blend quality before committing the production unit.
FAQ
Can a static mixer disperse pigment agglomerates in a coating?
No. It distributes the millbase and, for liquid–liquid systems, disperses droplets — CFD work on cross-bar elements ties droplet size to local energy dissipation in the lattice. Deagglomeration stays in the mill.
Which element geometry suits solvent-free, 100% solids coatings?
The laminar band favours cross-bar construction: the SX type covers 1–10,000 cP and reaches 1–5% non-uniformity with 4–6 elements, at 2–5 velocity heads per element. Pastes and hotmelts beyond 10,000 cP go to helical SK construction, which extends to 1,000,000 cP.
Why are two-component dispensing mixers treated as consumables?
The cure clock starts when components meet inside the element, and the cured material stays in the nozzle — so dispensing-side mixers are single-use. Production inline mixers avoid the waste but need planned flush protocols and quick element access.
What data does an engineer need to size a mixer for adhesive duty?
Each component's flow and viscosity at working temperature, the ratio window, line size and connections, available pressure drop, and the pot life. Viscosity ratio — not the blended average — stretches the required mix length.
Sources: Imperial College London, DNS study of surfactant-laden liquid–liquid dispersion in an SMX static mixer (droplet size vs local energy dissipation); Hernon, static mixers for two-component adhesive dispensing (elements combine components just before application); Sulzer SMV corrugated-sheet geometry (high-shear liquid–liquid dispersion duty); ywmixing published datasheet limits for SV, SX and SK types. Duty claims cite the cited sources and our own datasheets only.